From Implementation to Optimization: The Huffman Engineering MES Advantage
Key Highlights
- Process Knowledge Drives Success - Key input from operators prevents costly mistakes
- MES Delivers More Than Digital Records Real-time visibility, review-by-exception, data integrity, & faster quality decision-making define true MES.
- Optimization Creates Long-Term Value Improved critical process parameters, reduced quality issues, supported compliance, enabled advanced analytics, AI, & digital manufacturing initiatives are all optimized benefits.
Manufacturing Execution Systems (MES) have become a cornerstone of digital transformation across regulated and process-driven industries. While many organizations begin their journey by replacing paper records and digitizing workflows, the true value of MES lies in its ability to improve operational performance.
A MES provides visibility, control, and optimization of manufacturing operations through track and trace, inventory & maintenance management, document control, and production scheduling. By capturing and contextualizing data from people, equipment, materials, and processes, MES helps manufacturers answer critical questions:
- What are we producing?
- Which materials were used?
- Was the approved process followed?
- Are we in compliance?
- What happened during production?
Through real-time information, alarms, quality data, equipment states, and review-by-exception workflows, MES transforms operational data into actionable insights that improve quality, efficiency, compliance, and overall performance.
Some MES platforms are tailored to industries: life sciences, utilities, automotive, or energy, while others specialize in capabilities like Electronic Batch Records (EBR), batch recipe management, and procedure execution. MES solutions may also be built on specific SCADA vendors, cloud-native, or ERP-centric architectures, each offering different advantages in connectivity, scalability, and integration. Certified system integrators familiar with these differences help organizations find the best solution.
MES provides visibility, but its greatest value comes from turning production data into actionable information. MES creates a digital record of manufacturing activities that can be shared across operations, quality, maintenance, engineering, and business systems. What begins as a platform for data collection and traceability can evolve into a foundation for advanced analytics, OEE monitoring, predictive maintenance and intelligent scheduling.
At the shop-floor level, operators benefit from guided execution, automated recordkeeping, and review-by-exception workflows reducing training requirements, improving consistency, and minimizing compliance risks. By connecting data to decisions, MES enables manufacturers to continuously improve quality, efficiency, and operational performance.
Understanding the Process Before Technology
One of the most important steps in any MES implementation is gathering knowledge from the people who know the process best: operators, supervisors, and production personnel. These conversations reduce implementation timelines while minimizing costly surprises during deployment.
As teams dig deeper into the process, they often uncover inconsistencies, workarounds, and decision points that exist only as tribal knowledge. In many cases, experienced operators have developed informal methods to compensate for gaps in procedures, equipment limitations, or process variations. While these practices may keep production running successfully, they are rarely documented and can become points of failure when processes are standardized, automated, or executed by less experienced personnel. Identifying and addressing these hidden dependencies early helps ensure the MES accurately reflects how production should operate rather than how it has historically been kept running.
Organizations that skip this step often find themselves reworking workflows after implementation, leading to delays, additional costs, and reduced user adoption.
Preparing for a Smooth Transition
Effective MES deployment requires careful planning around downtime and implementation. Preparing documentation, updating policies and operating procedures, and aligning standards before the system goes live can significantly reduce disruptions and accelerate user adoption.
Planned downtime should be used strategically to perform system upgrades, validate system configurations, and prepare personnel for new workflows. Investing time in these activities early can prevent costly delays and implementation challenges later.
Visual inspections and process assessments also provide valuable insight before deployment. Key questions to consider include:
- What was the original process design?
- What is the process currently doing?
- How is performance and success measured?
- Where are the existing inefficiencies, bottlenecks, or sources of variation?
Answering these questions establishes a baseline for current operations and enables manufacturers to objectively measure improvements in efficiency, quality, compliance, and overall performance.
Moving Beyond Digital Records
Some organizations begin their MES journey with a focus on Electronic Batch Records (EBR) and the elimination of paper-based processes. While these benefits can provide significant improvements in compliance, traceability, and record retention, they represent only the first step in realizing the value of MES. A single balance is easy.
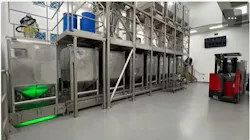
At Huffman Engineering we’ve seen this with projects at a global pharmaceutical facility known for its rapid production of common consumer health medications. Integrating feeders and balances with MES and SCADA allowed a manufacturing process to operate under PLC controls with MES setup and recording.
Our engineers designed and commissioned a fully automated batching and dispensing solution utilizing PLC controls and integrated measurement equipment. The system automatically weighed and dispensed materials from multiple bins, ensuring consistent product quality and compliance with established recipe and tolerance requirements.
As MES becomes integrated into daily operations, it evolves from a system of record into a system of execution and decision support. Production, quality, maintenance, and engineering teams gain access to consistent, real-time information that enables faster and more informed decisions. Review-by-exception workflows allow personnel to focus on deviations, alarms, and abnormal conditions rather than spending valuable time reviewing routine events.
As data accumulates, MES systems also provide the foundation for advanced analytics, machine learning applications, and artificial intelligence initiatives. Manufacturers can identify trends, anticipate issues, and make data-driven improvements that would be difficult or impossible using paper-based systems.
Enabling True Process Optimization
Collecting data is only the beginning of the MES journey. The greatest value is realized when that information is used to improve decision-making, standardize operations, and drive continuous improvement. An MES provides the visibility but the value is translating that insight into action.
Rather than simply documenting what happened, MES enables teams to monitor critical process parameters, identify sources of variation, and implement corrective actions before issues impact production. By connecting real-time operational data with quality, maintenance, and production objectives, organizations can:
- Detect quality issues earlier
- Respond to deviations more quickly
- Reduce batch losses and rework
- Improve Overall Equipment Effectiveness (OEE)
- Shorten investigation timelines
- Increase production consistency
- Standardize best practices across shifts and facilities
As organizations mature in their use of MES, the focus often shifts from recordkeeping and compliance to operational excellence. The system becomes a tool for driving continuous improvement, helping manufacturers reduce variability, optimize resource utilization, and achieve more predictable production outcomes.
Building a Foundation for Digital Manufacturing
MES serves as far more than a production tracking system. It becomes the digital backbone that connects manufacturing operations with analytics, reporting, cybersecurity initiatives, and future smart manufacturing technologies.
Electronic records stored within historians and connected systems provide secure, traceable documentation to support evolving compliance requirements and eliminates the risks associated with paper-based records. Manufacturers gain greater flexibility to manage recipe changes, enforce procedures, maintain audit trails, and ensure consistent execution across production lines and facilities.
MES also supports cybersecurity initiatives by providing controlled access to production data, role-based security, electronic audit trails, and integration with enterprise security policies. These capabilities help organizations improve visibility while maintaining the integrity and security of critical manufacturing information.
Ensuring that digital backbone remains strong is what the smart manufacturing journey is all about.
Sponsored By:
About the Author
Scott Woodward
Senior Systems Architect, Huffman Engineering
 Leaders Logo
Leaders relevant to this article: